Best Precision Steel Factory: Key Traits for Superior Manufacturing
2026-10-28
Precision steel isn’t just about hitting tight tolerances—it’s about trusting that every cut, bend, and finish will perform when it matters most. Too many buyers learn the hard way that not all factories deliver on that promise. So what actually separates a superior precision steel manufacturer from the rest? Shunchen steel has spent years refining the answer, and the traits below show exactly where to look before you commit.
Micron-Level Tolerances That Do Not Drift
Hitting a few microns on day one is easy. Keeping that same number after six months of thermal swings, vibration, and ordinary wear is another story entirely. The challenge isn't just cutting the part—it's building a system where every joint, guideway, and sensor behaves the same way at 6 a.m. as it does after a 14-hour shift.
Most drift comes from things people ignore: tiny differences in expansion between steel and aluminum, a ballscrew that warms up unevenly, or a feedback loop that's just a little too slow to catch a spike in load. The fix isn't a bigger motor or a tighter spec sheet. It's choosing materials that move together, mapping thermal behavior instead of guessing at it, and writing control algorithms that actively pull the axis back to where it belongs—before the error gets big enough to measure.
That's why the tolerance stays put over weeks and months, not just during a demo. The machine checks itself, compensates quietly, and keeps producing parts that match the print. No special climate-controlled room required. No weekly recalibration ritual. Just the same number on the gauge, again and again.
Alloy Consistency From First Pour to Final Coil
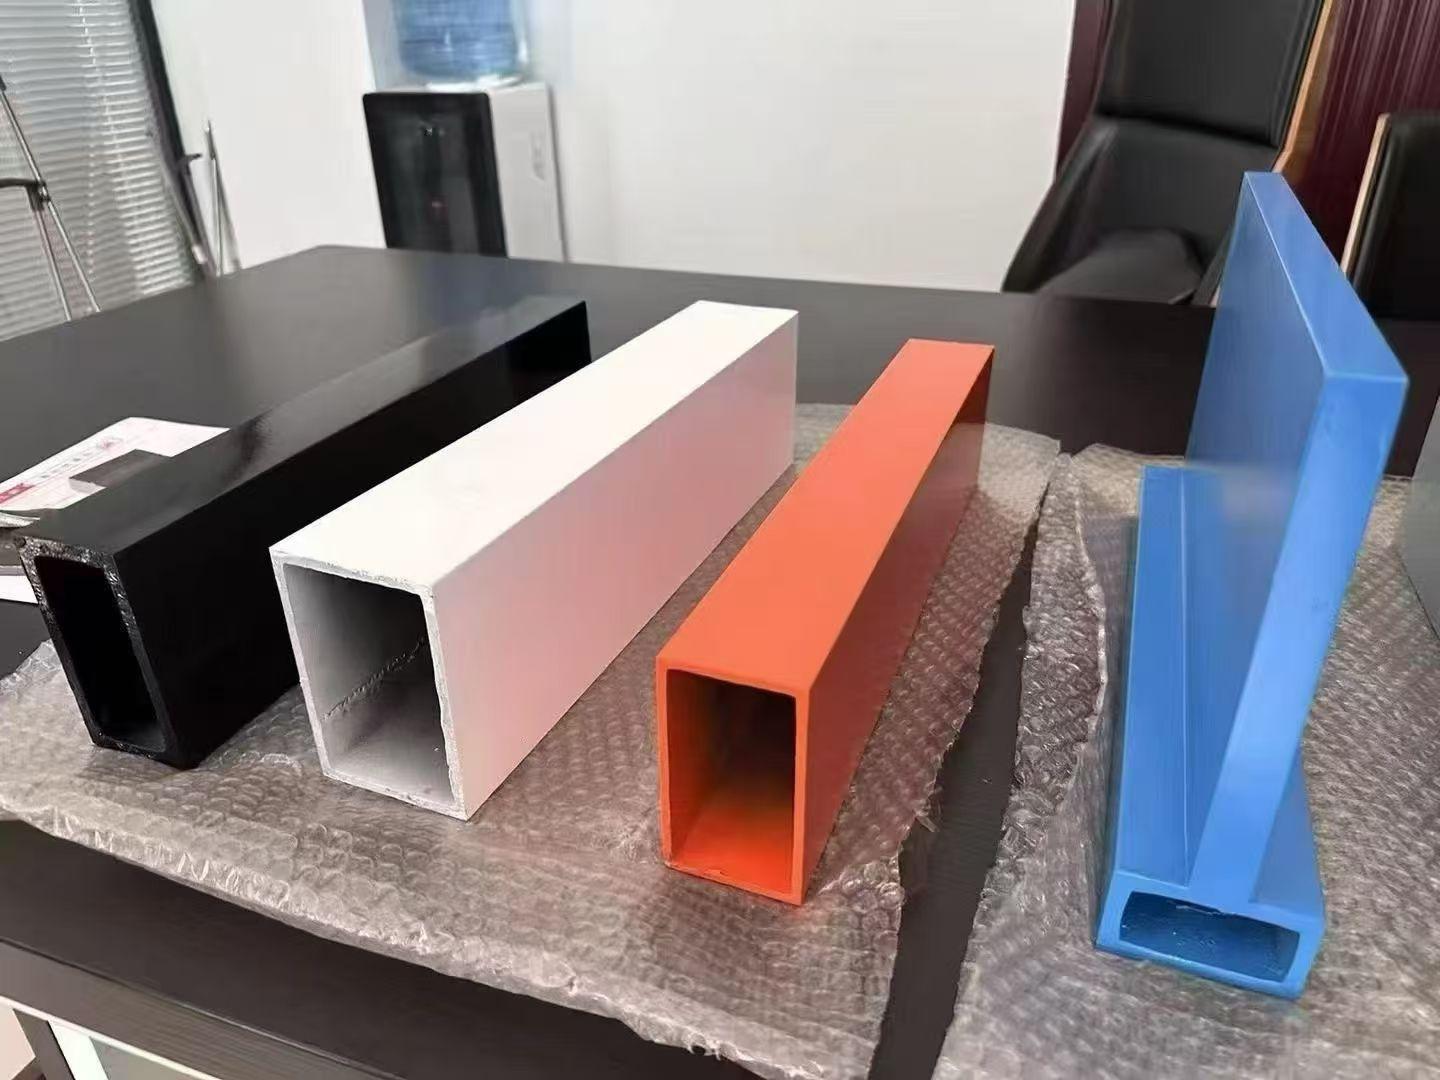
A lot can drift between the first pour and the last coil off the mill. We've learned to treat the melt deck not as a single snapshot but as a moving target. The chemistry from the spectrometer is only the starting point; the real test is how that melt behaves through the launder, across the casting tip, and into the solidifying strip. Small shifts in magnesium or silicon that still fall inside the spec can change how the metal work-hardens later, so we track every heat against its downstream coil properties rather than just its lab ticket.
The biggest consistency gains come from controlling what you cannot see: hydrogen pickup, oxide films, and the temperature gradient at the tip. If those are allowed to wander, you get a first coil that forms perfectly and a twentieth that tears at the same pass schedule. We run continuous degassing and ceramic foam filtration, but the real difference is keeping the headbox level and metal temperature within a few degrees across the entire cast. That stability lets the as-cast grain structure repeat from start to finish, so the mill sees the same strip coming in, hour after hour.
By the time the coil comes off the cold mill, consistency has already been earned upstream. We don't rely on re-rolling or selective sorting to fix chemistry drift. Instead, each heat is tied to its own cast length, and roll force signatures are compared against the first few coils of the campaign. When that signature stays flat—within the noise of the mill—you know the alloy held from first pour to final coil.
Heat Treatment That Reads the Steel, Not the Clock
Traditional heat treating cycles rely on fixed soak times, but steel batches vary enough that a stopwatch can lie. The newer approach tracks the steel’s actual response through magnetic permeability, thermal expansion, or internal friction. When the phase transformation completes, the recipe moves on—not because a timer says so, but because the material itself has signaled it is done.
This shifts the operator’s job from watching the clock to reading the steel. If a load arrives with slight differences in chemistry or section size, the process adjusts automatically. A thick casting and a thin forging might spend different times at temperature, yet both reach the same metallurgical state before quenching. That matters most in critical parts where an under-soaked core or an over-tempered surface is not acceptable.
The benefit is less rework and fewer surprises in hardness testing. Instead of assuming every batch behaves like the last, the furnace responds to what is actually happening inside the steel. It is a quieter kind of precision—one that treats each load as its own problem rather than a fixed recipe to be repeated.
The Reject Pile Stays Small for a Reason
A slim reject pile fools people into thinking the work arriving is uniformly strong. It rarely is. The real reason it stays small is that the first cut happens fast, often before a full read. Weak openings, vague premises, or a mismatch with the publication's tone get removed within minutes.
That speed creates a feedback loop. Writers who notice their work bounced early stop submitting half-formed drafts. They test the central idea, sharpen the first paragraph, and only send what fits. The pile shrinks because the threshold for staying in consideration is clear, not because fewer people are writing.
There is also a hidden benefit: a small reject pile keeps decisions sharper. When an editor can remember every piece they passed on in a week, patterns emerge. They see what near-misses look like and can adjust guidance. The pile stays manageable, but it never becomes stale.
Custom Profiles Without the Custom Headaches
Most "customizable" tools make you earn the label. You wade through parameter lists, edit config files by hand, and pray an update doesn't wipe out your tweaks. What starts as a simple preference change turns into a half-day project, and eventually you stop customizing entirely because the payoff isn't worth the pain.
This platform takes the opposite approach. Instead of handing you a blank text editor and wishing you luck, it gives you a library of pre-built profile blocks that snap together. Pick your triggers, set your thresholds, drag a slider or two—done. The underlying structure stays clean, so when versions change, your custom profile migrates without breaking a sweat.
The result is all the upside of a bespoke setup—faster navigation, fewer repetitive clicks, layouts that actually match how you think—without the usual maintenance burden. You don't need to be a power user. You don't need to keep notes on what line 47 does. You just tweak what matters, leave the rest alone, and get back to work.
Promised Friday Means Friday, Not Monday
Few things erode trust faster than a deadline that quietly slips to Monday. When you say Friday, people arrange their own work around that word, not just their schedule but their expectations. Changing it later, without a real emergency, sends a message that their planning never mattered much to you.
The disappointment of a Friday promise turned into Monday's apology lingers long after the work itself is delivered. The quality may be fine, but the shine is gone. What people remember is how the delay made them feel: small, unheard, and forced to adjust because someone else couldn't keep a simple date.
Protecting Friday isn't about rigidity; it's about making your word something others can build on. If the timeline feels tight, say Wednesday. If you commit to Friday, treat it like an appointment with someone you cannot afford to lose. Friday means Friday, not a Monday surprise.
FAQ
The difference often comes down to consistent dimensional control at tight tolerances, along with the ability to repeat that precision across large production runs. A top-tier factory will also carry in-house metallurgical expertise, allowing it to adjust alloy composition and heat treatment to match the final component's stress conditions.
Look beyond basic cutting and forming. Strong candidates typically offer cold rolling, precision slitting, annealing, and surface finishing under one roof. That reduces hand-off delays and gives the factory full ownership of quality from raw coil to finished blank.
It is often the quiet determinant of quality. Mills that control their sourcing or work with a short list of audited steelmakers can trace every batch back to its heat number, making it easier to isolate variations in hardness, grain structure, or coating adhesion before they reach final parts.
The best operations treat quality control as a forensic process, not a final gate. They use coordinate measuring machines, surface profilometers, and tensile testing to map how a coil performs from edge to edge. That data feeds back into roll adjustment and thermal profiles, reducing drift over time.
Yes, but only if the shop floor is built for flexible scheduling. Look for factories that use quick-change tooling, shared die libraries, and modular processing lines. These allow short runs to move through the same tight tolerance controls as mass production, instead of being pushed to a separate, less disciplined line.
Request a first-article inspection report with actual measured values, not just a certificate that says 'pass.' Better yet, ask for a small pilot batch and have it checked independently. Factories confident in their process will agree to this because they know the numbers will match their internal data.
The obvious costs are scrap and rework, but the deeper ones include downstream assembly failures, warranty claims, and fatigue-related field breakdowns. A steel part that is slightly out of flatness or has inconsistent hardness may look fine at receiving inspection and still cause problems months later.
In-line laser gauging and automated surface inspection now catch deviations in real time, while digital twin simulations let engineers test roll gap and cooling changes without disrupting production. These tools move precision from sample-based checks toward continuous, closed-loop control.
Conclusion
A precision steel factory earns its name through what you cannot see on the surface. Micron-level tolerances have to hold across thousands of parts, not just the first ten off the line, and that discipline comes from tooling maintenance schedules, in-process laser checks, and an almost stubborn refusal to accept drift. Alloy consistency depends on more than a decent recipe; every heat is verified from the first pour to the final coil, with spectrographic readings logged against the supplier's certified chemistry. Heat treatment, too, is treated as a conversation with the material. The steel's own temperature curve and grain response decide how long it stays in the furnace—not a timer that someone set once and forgot.
That same rigor shows up further down the line. A small reject pile is not luck; it means operators stop and correct a tool offset before it becomes a bad batch, and every questionable strip is pulled for rework instead of being shipped with a shrug. When customers need custom profiles, the best shops keep a library of proven roll-forming setups and involve the engineering team early, so a special shape does not trigger a month of trial-and-error. And delivery dates are treated as part of the specification. If a factory says Friday, the truck is loaded and the paperwork is ready by Thursday afternoon—because precision in manufacturing means nothing if the schedule itself is allowed to slip.
Contact Us
Contact Person: Max Zhou
Email: [email protected]
Tel/WhatsApp: +86 15712216177
Website: https://www.shunchensteelmaterial.com/