HC-22 Nickel Based Alloy Extruded Seamless Pipe Company You Can Trust for High-Performance Alloys
2026-10-31
Sourcing HC-22 nickel based alloy extruded seamless pipe? The real challenge isn't finding a supplier—it's finding one that treats high-performance alloys as more than a commodity. JILAIDA has earned trust by proving its HC-22 seamless pipe performs where corrosion and extreme temperatures push ordinary materials to failure. That track record is exactly what this post digs into.
Inside HC-22: The Alloy Behind Demanding Pipeline Systems
HC-22 emerged as a direct response to the failure points of conventional stainless grades in aggressive chloride-bearing environments. Where 316L pits and crevice corrosion take hold within months, this nickel-chromium-molybdenum alloy holds its surface integrity through a carefully balanced microstructure. The high molybdenum content works alongside chromium to form a passive film that resists breakdown even in hot, acidic brines—conditions that quickly degrade lesser materials. Field data from sour gas processing units shows wall thickness loss rates under 0.05 mm/year, often an order of magnitude better than duplex alternatives in the same service.
One overlooked advantage is how HC-22 behaves during welding and post-weld heat treatment. Unlike alloys that require exotic filler metals or risk sensitization at the heat-affected zone, HC-22 maintains its corrosion resistance across a wider range of heat inputs. This gives fabricators more room to maneuver on site without sacrificing long-term reliability. Several offshore operators have adopted it specifically for flare lines and produced water reinjection piping, where intermittent wetting and high temperatures create unpredictable local chemistries. The alloy's resistance to both oxidizing and reducing media means it doesn't demand the same degree of process control that titanium or super duplex often impose.
Cost comparisons often miss the full picture. While HC-22 carries a higher initial price per meter than standard 304 or 316, its lifecycle economics shift when replacement downtime, inspection frequency, and unplanned shutdowns are factored in. A single avoided leak in a buried pipeline—where excavation and repair can exceed the pipe cost tenfold—justifies the premium. Engineers specifying HC-22 for demanding pipeline systems typically report lower total installed cost after five years, driven less by material price and more by the absence of corrosion-related interventions. That operational quietness is the real value proposition.
Why Extruded Seamless Pipes Change the Equation for Corrosive Environments
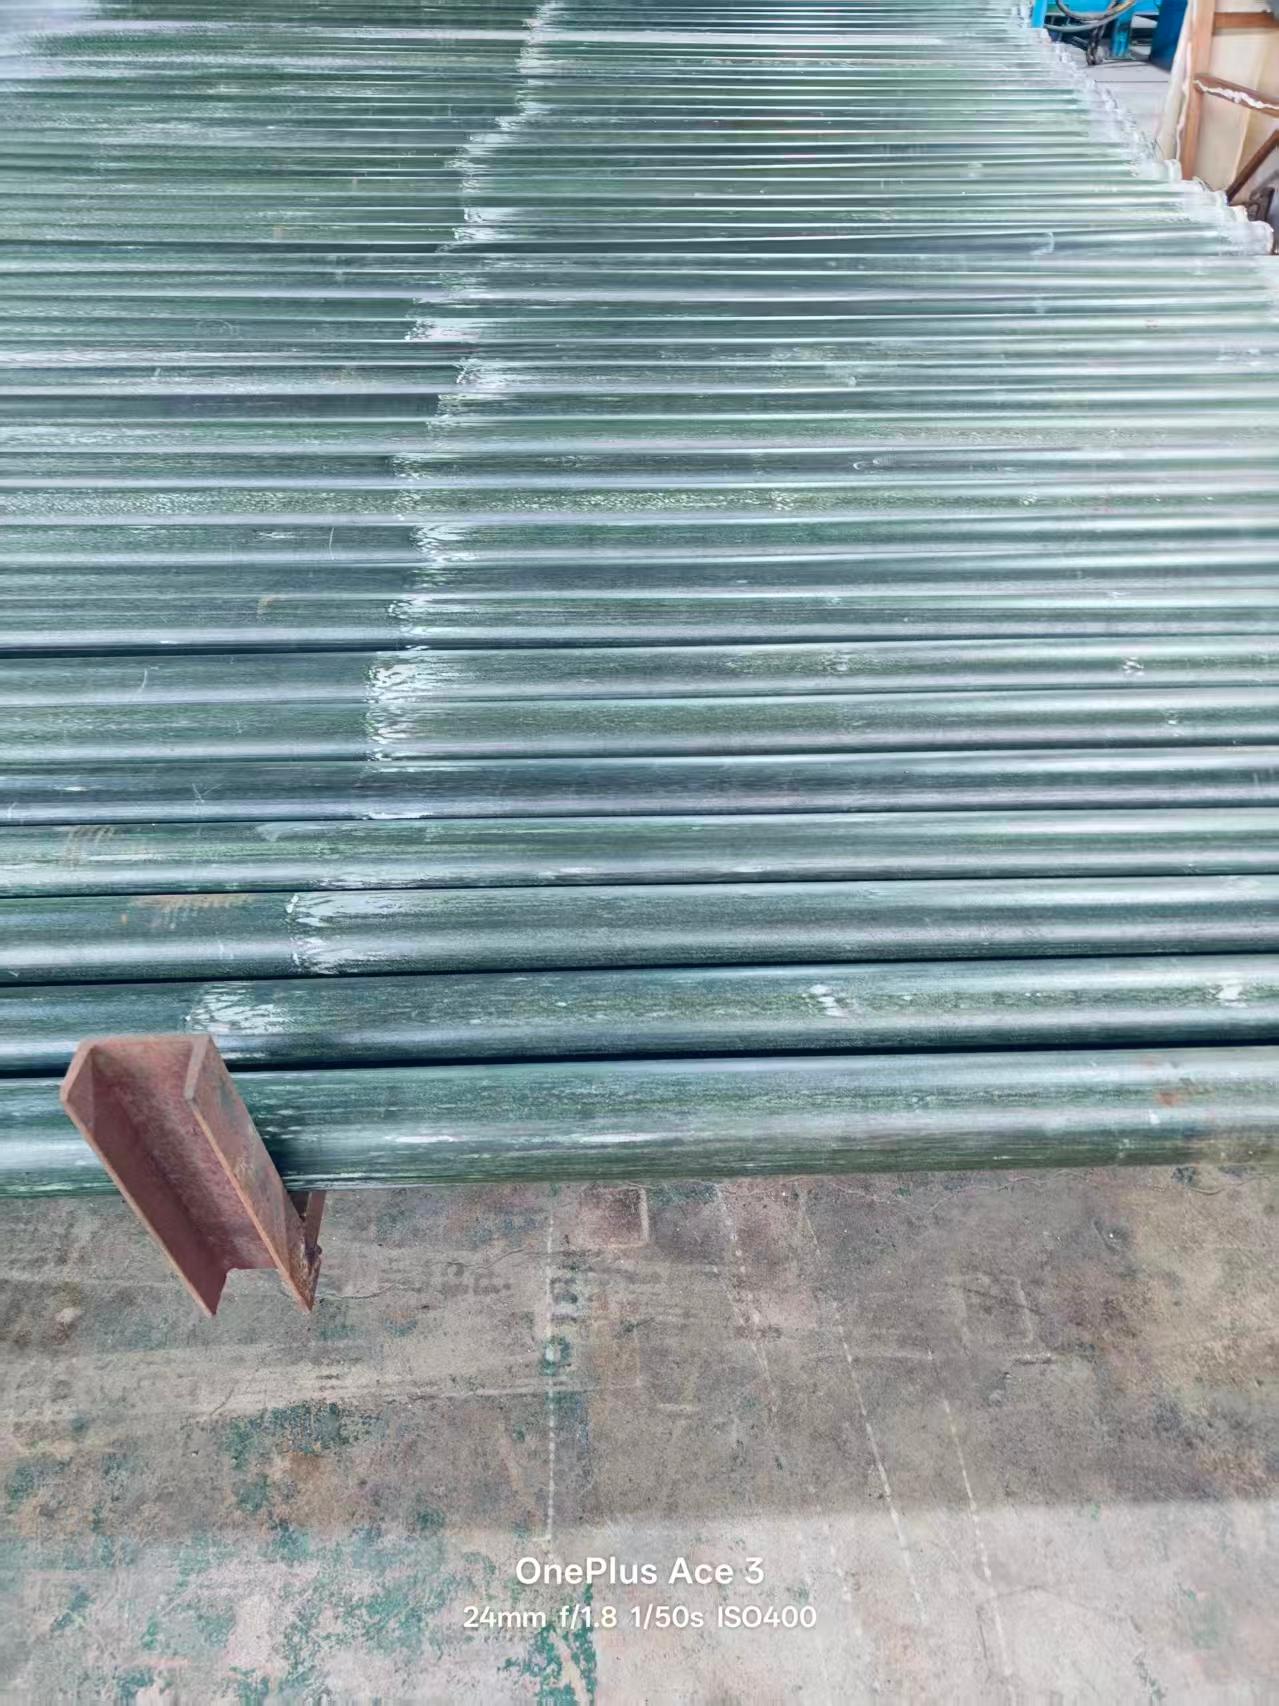
Extruded seamless pipes eliminate the longitudinal weld seam that typically becomes the weak link in corrosive service. Without that heat-affected zone, the grain structure remains uniform around the entire circumference, so there’s no preferential path for pitting or stress-corrosion cracking. This matters most in chloride-heavy or sour environments, where a single micro-fissure can turn into a full-bore failure within months.
The hot extrusion process also lets mills use higher-alloy materials that resist corrosion better but are difficult to form by other methods. Nickel alloys, duplex stainless steels, and titanium grades flow more predictably under the severe deformation of extrusion, resulting in a homogeneous microstructure with fewer inclusions. Operators get a pipe that holds up against acids, seawater, and aggressive chemicals without the constant patching and downtime that welded alternatives often demand.
From Melt to Mill: How Our HC-22 Pipes Take Shape
The whole process starts with a charge of nickel, chromium, molybdenum, and tungsten going into the furnace under tight atmospheric control. The melt is sampled before tapping, and the heat is not released until the HC-22 chemistry sits inside a narrow band. That early discipline keeps later forming steps from amplifying small variations into out-of-spec pipe.
After tapping, the alloy is cast into round billets or hollow shells, then moved through a reheat furnace. The first rolling passes are not about final size; they are about breaking down the cast structure and closing any porosity left from solidification. Operators watch the reduction ratio carefully, because too little work leaves a coarse grain that can hurt both strength and corrosion performance.
The final shape comes from cold pilgering or cold drawing, with wall thickness and ovality checked after every pass. Lubrication, tooling speed, and feed rate are adjusted on the fly rather than set once and forgotten. By the time the pipe reaches its finished dimensions, it has carried the same controlled chemistry and worked microstructure from the melt all the way to the mill floor.
Standards That Matter: Traceability and Testing Without Shortcuts
Traceability is often treated as a bureaucratic exercise, but in practice it is the difference between catching a contaminant before it leaves the facility and recalling an entire season's worth of product. For any producer serious about quality, a lot code must lead back to the exact field harvest date, processing line, and even the operator shift. That level of granularity doesn't happen by accident; it requires barcode or RFID systems that log every handoff, not just the final pallet. When something goes wrong, the question is not whether you can produce a spreadsheet, but whether you can isolate the affected batch in under an hour.
Testing without shortcuts means rejecting the temptation to sample only the easiest points in a process. Incoming raw material checks, in-line verification, and finished product assays each catch different failure modes. A facility that skips viscosity testing on a coating, for example, may ship product that looks fine on the bench but fails after three months of thermal cycling. The standard that matters is not the number of tests performed, but whether the test plan mirrors the actual risks: microbial growth, chemical drift, dimensional tolerance, or material fatigue. If a test can be gamed by tweaking a single variable, it is not a control, it is theatre.
The real burden falls on leadership to resource these systems properly. Traceability software that no one updates is worse than a paper log, because it gives a false sense of control. Calibrated instruments, trained technicians, and unannounced audits all cost money, but they cost far less than a recall, a lawsuit, or a broken customer relationship. Shortcuts accumulate quietly until a single failure exposes the gap. Standards only matter when they are enforced on a Tuesday afternoon, not during a pre-certification walkthrough.
Real-World Service Life: HC-22 in Refining and Chemical Processing
Refinery operators often measure service life not in years, but in shutdown cycles. HC-22 components—valve trim, thermowells, injection nozzles—sit in the path of hot, sour crude fractions where naphthenic acid and hydrogen sulfide conspire against lesser alloys. Field reports from Gulf Coast crude units describe HC-22 piping still within corrosion allowance after seven years of continuous exposure, while adjacent 316L spools required replacement after two. The difference comes down to the alloy's ability to hold a passive film under alternating carburization and sulfidation conditions, a scenario that routinely destroys conventional stainless steels.
Chemical processors handling chlorinated organics, mixed acid streams, or hot ferric chloride solutions face a similar calculus. Here, HC-22 earns its keep in heat exchanger tubing and reactor internals where pitting and crevice attack are the dominant failure modes. One Midwest specialty chemical plant documented HC-22 tube bundles surviving 90,000 hours in a reactor effluent cooler—conditions that had previously forced retubing every 18 months with alloy 625. The nickel-chromium-molybdenum balance of HC-22 provides the critical pitting resistance equivalent number needed to shrug off localized attack that would chew through lesser C-type alloys.
What separates HC-22 from other corrosion-resistant alloys is not a single magic property, but the way its performance holds up when process upsets occur. Startups with wet chloride condensation, shutdowns with residual acid films, temperature excursions beyond design limits—these transient events drive most real-world failures. HC-22's generous molybdenum and tungsten content, combined with its controlled iron level, gives it a wider operating window before repassivation becomes impossible. For maintenance engineers, that translates into fewer unplanned inspections and more confidence extending time between turnarounds.
Choosing a Supplier Who Understands High-Temperature Integrity
Selecting a supplier for high-temperature applications goes beyond checking a spec sheet. The materials, coatings, and assembly methods must hold up when temperatures climb, but the real test is whether the supplier understands how thermal cycling, oxidation, and creep interact in your specific operating environment. Look for a partner who asks about your peak temperatures, dwell times, and cooling rates before recommending anything. A supplier who simply quotes a maximum service temperature without discussing the full thermal profile is likely missing the point.
You can often tell how deeply a supplier grasps high-temperature integrity by the questions they raise. Do they ask about thermal gradients across a component? Are they concerned about embrittlement after long exposure or the stability of fasteners at elevated heat? A knowledgeable supplier will walk you through trade-offs between different alloys, ceramic coatings, or sealing methods, and they won't hesitate to point out where a lower-cost material might fail prematurely. That kind of candor saves more than money—it prevents unplanned shutdowns.
Finally, verify that the supplier has hands-on experience with your industry's thermal demands, not just a generic catalog. Ask for case studies or examples where they solved a high-temperature integrity problem similar to yours. A supplier who has seen field failures and adjusted their approach understands that high-temperature performance is not a static property but a behavior that must be managed over the entire life of the part.
FAQ
Extruded seamless pipe eliminates the longitudinal weld seam, which is often the weakest point in aggressive chemical environments. HC-22's nickel-chromium-molybdenum composition already resists pitting and crevice corrosion, and removing the weld zone means you don't have to worry about sensitization or inconsistent grain structure along a seam. That translates to fewer premature failures in reactors, heat exchangers, and downhole equipment where chloride-rich media are present.
Chemical processing, pharmaceutical manufacturing, and oil and gas extraction rely on it heavily. For instance, in a flue gas desulfurization system, the combination of sulfuric acid condensation and high temperatures quickly eats through standard stainless steel. HC-22 seamless pipe holds up because its high molybdenum content provides excellent resistance to both oxidizing and reducing acids, extending replacement intervals from months to several years.
Extrusion works the billet under high pressure and controlled temperature, which refines the grain structure more uniformly than roll forming. The result is a denser, more homogeneous pipe wall with consistent mechanical properties around the entire circumference. For HC-22, this is critical because even minor segregation of alloying elements can create localized weak spots in severe service.
HC-22 performs well from cryogenic temperatures up to about 1250°F (677°C) in oxidizing environments. It retains toughness at low temperatures and resists scaling and carburization at elevated temperatures, though prolonged exposure above 1250°F may reduce its ductility. For most chemical and petrochemical applications, it offers a much wider operating window than 316L stainless or duplex grades.
The company focuses exclusively on high-performance nickel alloys and uses in-house extrusion capabilities, which gives it direct control over wall thickness tolerance, surface finish, and heat treatment. They also provide full material traceability, including melt source and mechanical test reports for each heat. That level of transparency is rare among general pipe distributors and matters when a failed pipe can shut down an entire unit.
Yes, HC-22 is one of the most seawater-resistant nickel alloys available. It withstands stagnant seawater and high-chloride brines better than C-276 and far better than super duplex stainless steels. However, under severe fouling or where crevices are unavoidable, a periodic flush or cathodic protection is still recommended to maximize service life.
Depending on the production run, the company can supply outside diameters from 1/2 inch to 8 inches (12.7 mm to 203.2 mm) with wall thicknesses as light as Schedule 10S and as heavy as Schedule 160 or beyond. Custom non-standard sizes are also possible because the extrusion tooling is more flexible than welded pipe manufacturing.
Conclusion
HC-22's metallurgical profile sets it apart in demanding pipeline systems—its nickel-chromium-molybdenum matrix withstands aggressive chlorides, reducing acids, and oxidizing media that quickly degrade standard stainless grades. Extruded seamless construction removes the weak points of welded pipe, eliminating longitudinal seams that often fail first in corrosive service. The result is a pipe that holds up under thermal cycling, stress corrosion cracking, and pitting in refineries and chemical plants.
From precise melt chemistry to hot extrusion and cold pilgering, every step is controlled to produce a homogeneous grain structure and consistent wall thickness. Traceability is not an afterthought: each heat is verified against ASTM/ASME specifications, with full documentation of mechanical testing, ultrasonic inspection, and positive material identification. In real-world service, HC-22 pipes routinely outlast conventional alloys in harsh acid services and high-temperature reactors, reducing unscheduled shutdowns and replacement costs. Choosing a supplier who understands high-temperature integrity means working with engineers who can advise on alloy selection, fabrication, and long-term performance—not just a vendor shipping stock.
Contact Us
Contact Person: Chenji Li
Email: 521 Zhonghui Road, Huishan Economic Development Zone
Tel/WhatsApp: +86 83112233
Website: https://www.jldnickelalloy.com/