How to Select a Top-Quality Aluminum Cylinder Head Supplier for Your Engine Build
2026-07-19
Selecting the right aluminum cylinder head supplier can make or break your engine build. With so many options promising high flow and durability, how do you separate genuine quality from empty claims? At DDR, we’ve seen what truly defines top-tier craftsmanship—and what doesn’t. This guide cuts through the noise, giving you the practical insights needed to choose a partner that meets the demands of your performance goals.
Beyond the Brochure: Spotting Genuine Craftsmanship
Flip through any glossy brochure and you'll find the same promises: ‘artisan-made,’ ‘handcrafted quality,’ ‘built to last.’ But how much of that language holds up when you run your fingers along the seams? True craftsmanship doesn’t shout—it reveals itself in the quiet details. Look beyond the marketing copy. Check the weight of a handle, the fit of a joint, the way light catches a surface without revealing sanding marks or rushed finish work. These are the signals that separate careful human touch from machine precision dressed up in heritage buzzwords.
One reliable test is to hunt for the imperfections that signal intention. A perfectly uniform piece might have been churned out by a CNC router, while a subtle, irregular chamfer or a gently pillowed edge suggests a craftsperson who made deliberate choices about feel and function. Peer inside drawers and cabinets—are the secondary woods chosen with care or are they afterthoughts? Run a finger along the underside of a table. If it's rough and unfinished, you're looking at cost-cutting, not tradition. Genuine work tends to show respect even in the places no one thinks to inspect.
Finally, ask about materials and joinery in a way that invites a story. A real craftsperson will light up explaining why they chose quartersawn oak for stability or how a dovetail angle was tweaked to suit a particular drawer depth. If you get a rehearsed sales pitch instead of enthusiasm, that's a brochure talking, not a maker. Objects made with integrity carry a sense of time—the years it took to master a technique, the hours poured into a single piece. You’ll feel it in the balance of a chair, the warmth of a hand-planed surface, the quiet confidence that this thing will outlast the trends. After all, a brochure fades, but craftsmanship stays in the bones of a piece long after the hype is gone.
The Metallurgy Behind Peak Performance
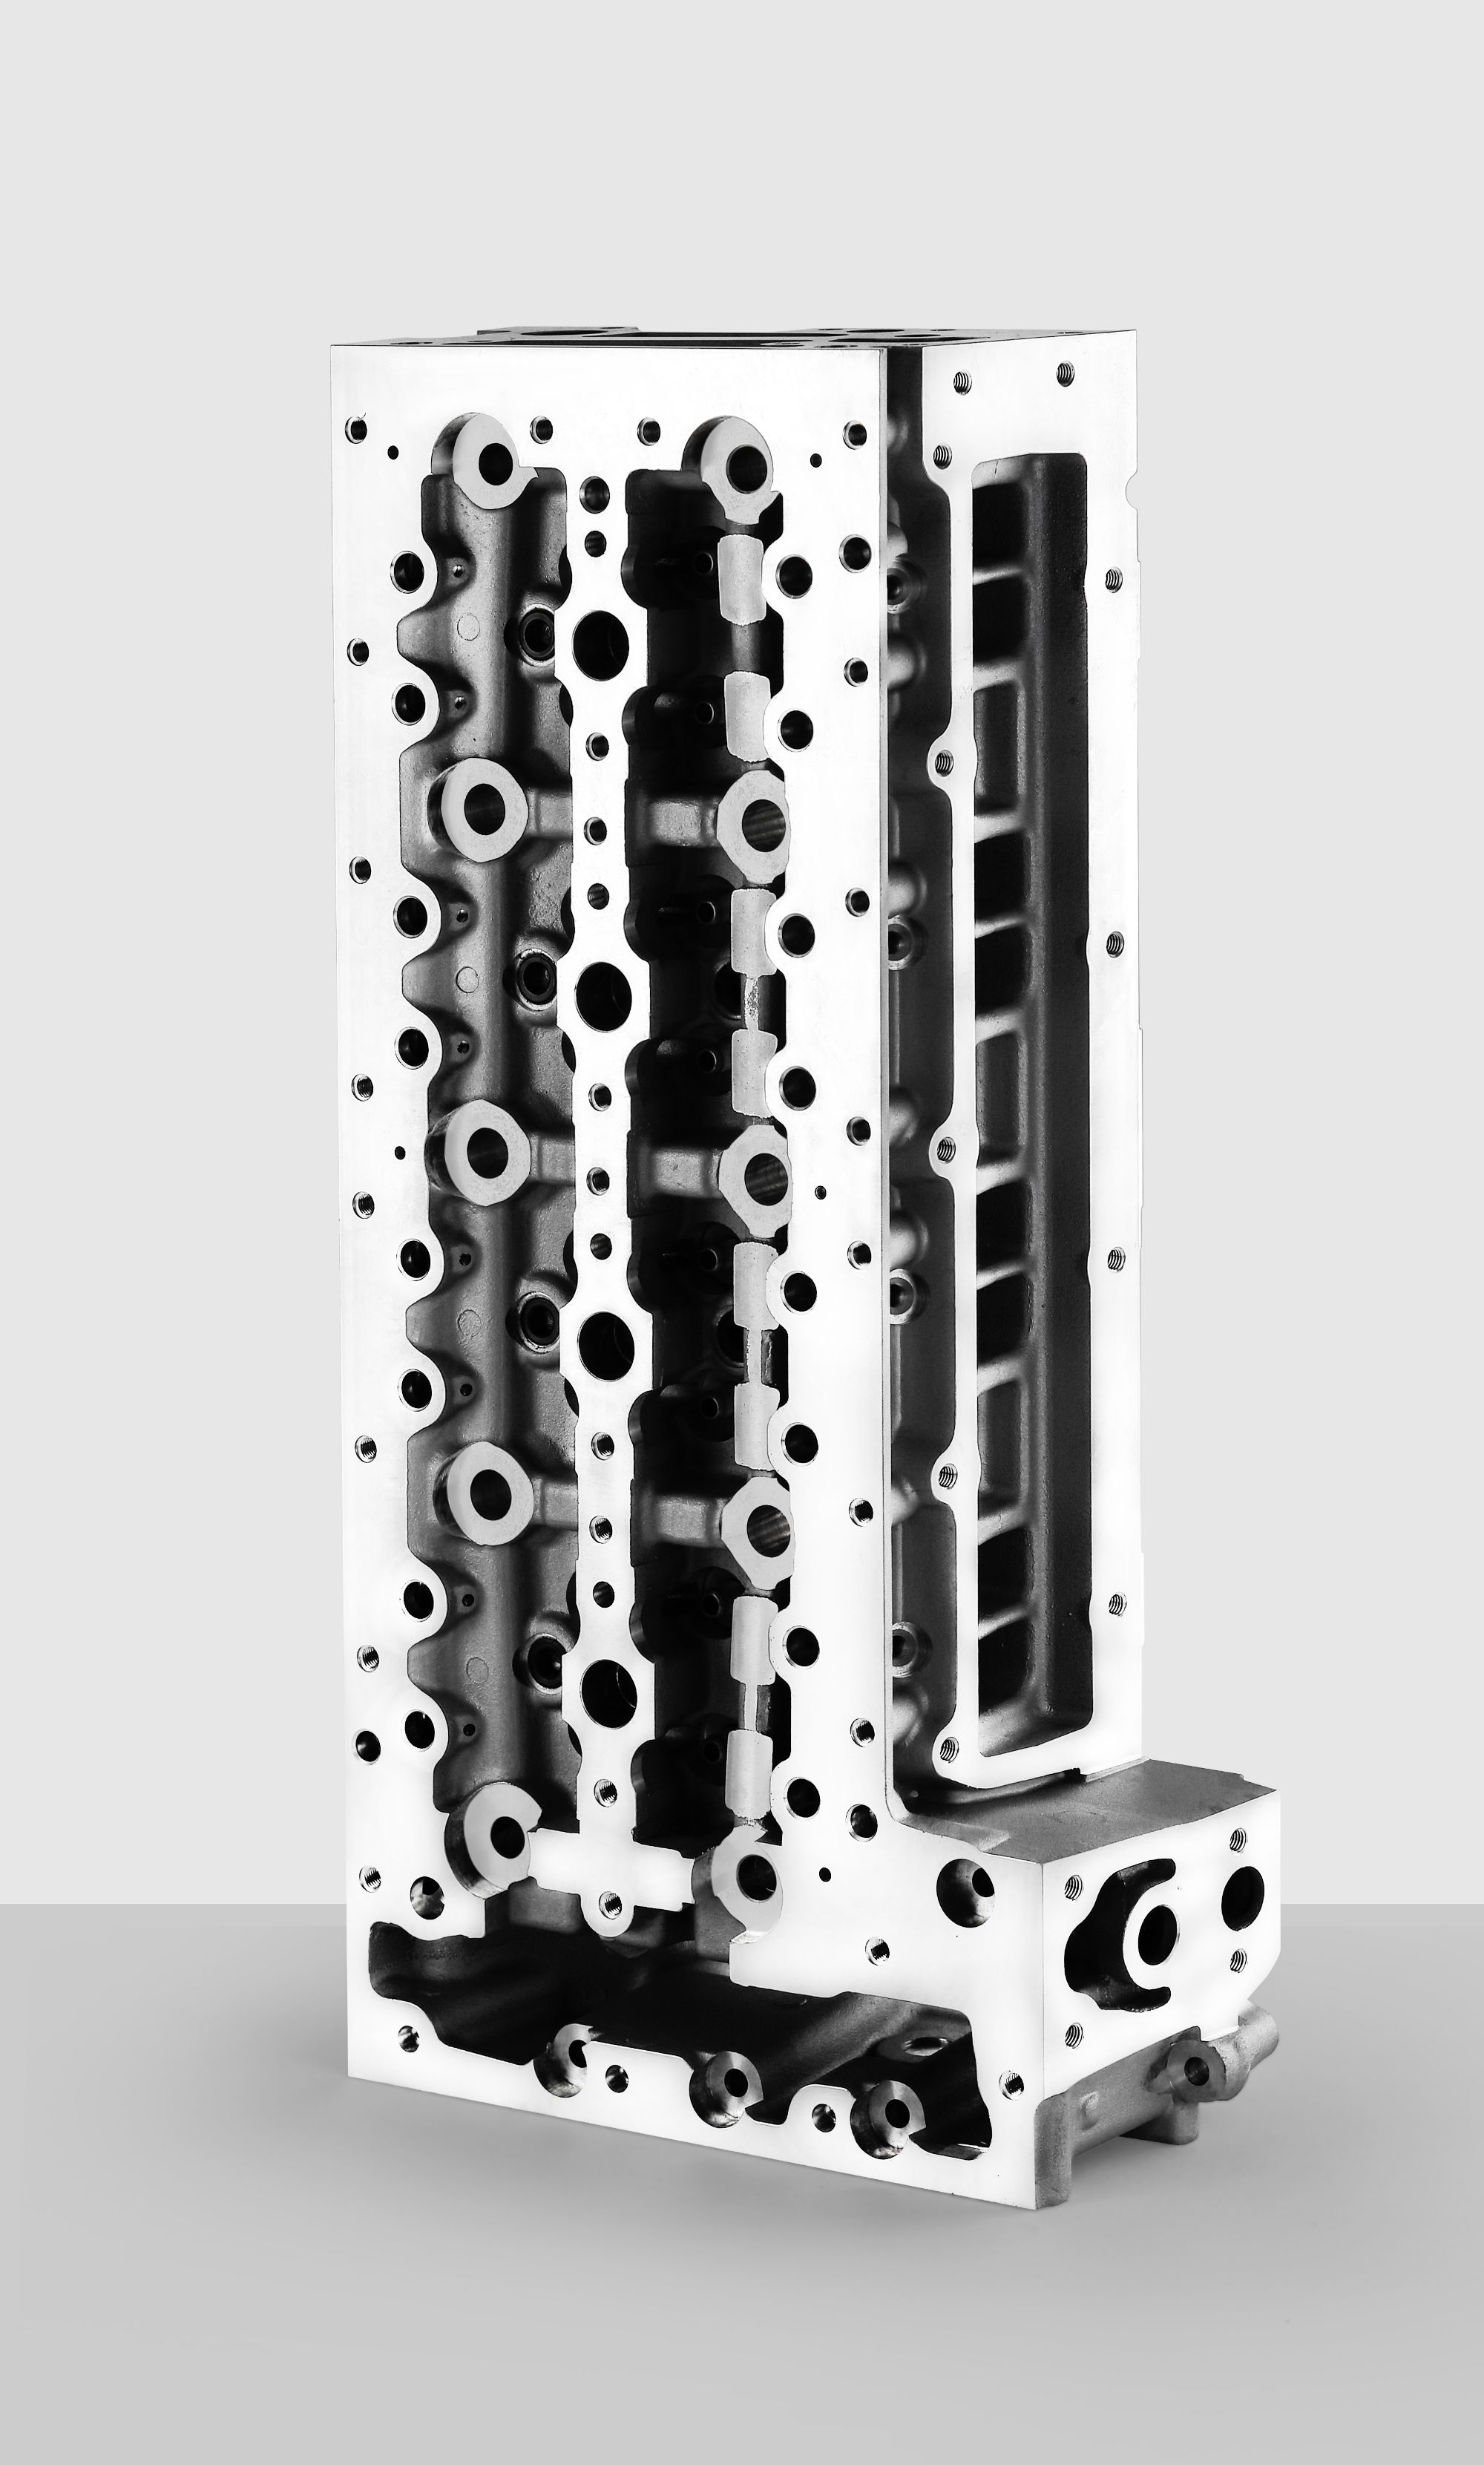
Every champion piece of equipment—whether a cyclist’s frame, a surgeon’s scalpel, or a jet engine turbine—owes its edge to decisions made at the atomic level. The real magic isn’t in choosing titanium over steel, but in manipulating how atoms arrange themselves during cooling, how dislocations move under stress, and how microscopic precipitates pin those dislocations in place. A slight tweak in aging temperature can transform a brittle alloy into one that flexes without fracturing, absorbing shock while staying impossibly light. It’s a silent, invisible dance that happens in furnaces and quenching baths long before the final product ever sees a racetrack or an operating room.
Take the finest golf club faces, for instance. They don’t just need to be hard—they need to spring back with explosive efficiency, transferring energy to the ball without shattering. That’s where maraging steels come in, their strength born not from carbon but from nanoscale intermetallic compounds that form during careful heat treatment. The result is a material with the resilience of a premium spring and the durability to withstand thousands of violent impacts. In other arenas, the story repeats with different actors: beta titanium alloys in orthopedic implants that flex with bone rather than shielding it from stress, or single-crystal superalloys in jet engines that defy creeping deformation at temperatures that would turn lesser metals soft. Each breakthrough isn’t magic—it’s metallurgy, tuned to the specific rhythm of peak performance.
Yet what separates good components from truly elite ones often lies in the imperfections, not the purity. Controlled inclusions, deliberate grain boundary engineering, and even the way a metal is forged can channel stresses away from weak points. A Formula 1 team doesn’t just want a strong suspension arm; they want one that bends slightly under load to communicate feedback to the driver, then regains its shape without fatigue. That requires a metallurgist to think less like a chemist and more like a composer, orchestrating a symphony of phases—martensite here, retained austenite there—to deliver strength, ductility, and a touch of controlled elasticity. When it all clicks, the metal itself becomes an active partner in the pursuit of victory, not just a passive slab of material.
When a Supplier Becomes Your Engineering Partner
When a supplier starts thinking like an engineer, the relationship shifts from transactional to transformational. Instead of simply delivering parts to a spec, they begin asking the right questions: Why this material? What’s the stress point? Could a different geometry reduce weight without sacrificing strength? This proactive curiosity often uncovers optimizations that a purely in-house team might miss, simply because the supplier brings a broader view of manufacturing possibilities and real-world constraints. They combine deep material knowledge with production-floor insights to propose alternatives that improve performance, cut costs, or both.
A true engineering partner doesn't just react to problems—they help you avoid them in the first place. Early collaboration during the design phase allows them to flag potential manufacturing headaches, suggest design for assembly tweaks, or recommend off-the-shelf components that eliminate custom tooling. It's not about second-guessing your engineers; it's about layering their specialized expertise onto your vision. Over time, this shared problem-solving builds a level of trust where they feel comfortable challenging assumptions and proposing innovations that push your product forward.
The best part? This partnership accelerates iteration. When your supplier understands not just what you're building but why, they can prioritize your prototypes, flex their schedule for urgent testing, and even contribute design improvements on the fly. Instead of a siloed handoff, development becomes a continuous, collaborative loop—prototype, test, refine—where the supplier is a key contributor to the final design. That's when you stop having a vendor and start having a competitive advantage.
Stress-Tested and Track-Proven: What to Look For
When a component claims to be stress-tested and track-proven, you’re essentially looking for evidence of relentless punishment and survival. It’s not about lab simulations that follow a neat script—it’s about the chaotic, violent forces that only real track sessions can dish out. Heat soak from repeated high-speed laps, sustained lateral loads that twist chassis and suspension parts, and the shock of curbing that sends jolts through every weld and fastener. The best parts aren’t just designed to handle these; they’ve proven it over hundreds of laps without deformation, fatigue cracks, or degradation in performance. Look for telltale signs like detailed heat-cycling records, third-party race team endorsements, and data logs showing consistent performance after prolonged abuse. If the manufacturer can’t show you a dyno sheet or bore scope image after a 24-hour endurance run, assume the “track-proven” label is just marketing fluff.
Materials matter more than glossy advertising. A stress-tested part should reveal its metallurgy proudly—whether it’s forged 7075 aluminum, chromoly steel with proper heat treat, or a composite that’s been autoclave-cured. Track-proven means the raw ingredients have been cooked in a racing environment where failure isn’t an option. Check for mill certs, hardness test results, and notes on grain structure from the forging process. On the track, repeated cycles flex components in ways a single dyno pull never will, so look for design features that specifically address fatigue resistance—shot-peened surfaces, radiused edges in high-stress areas, and FEA models that were validated with actual telemetry data. If the part has been used in sanctioned competition series, that pedigree matters because series rules often force engineers to push reliability boundaries within strict material limitations.
Finally, don’t overlook the importance of transparency in testing methodology. True track-proven components are often accompanied by detailed build logs, inspection intervals, and photographic evidence of the part in action. A stress test that matters goes beyond simply maxing out a hydraulic ram; it involves mounting the part on a dedicated test mule car, running slicks on a grippy circuit, and then tearing everything down to measure runout, crack length, or bushing compliance. The best companies will share footage of this process, and the most telling detail isn’t the peak force a part handled—it’s how much performance it retained after a full season of sprint races. When evaluating, ask for the post-season teardown report: if the bearing bores are still round and the threads haven’t stretched, you’re on the right track.
Building Relationships That Last Beyond the First Order
A single transaction rarely tells the full story. What starts as a first order should be seen as an opening chapter, not a closed deal. To truly connect, you need to move beyond the invoice and start understanding the person behind the purchase. Ask questions that reveal their long-term goals, not just their immediate needs. When a customer feels genuinely heard, their loyalty isn't bought—it's built over time through shared understanding and authentic interest.
The real magic happens in the moments between orders. A thoughtful check-in when nothing is due, a helpful resource shared without a sales pitch, or a quick note on something they mentioned months ago—these small, human touchpoints signal that you value the relationship, not just the revenue. Consistency here matters more than grand gestures. It’s about showing up reliably with relevance and care, turning a transactional connection into a trusted partnership that naturally leads to repeat business.
Ultimately, relationships outlast any single product or price tag. When you invest in honest communication, flexibility when things go sideways, and a willingness to go beyond the expected, customers become advocates. They return not because of a loyalty program, but because they know you have their back. This kind of trust isn’t manufactured—it’s earned through every interaction, making the next order a natural step in a long-term journey together.
FAQ
Start by looking at their track record. Ask for client references in your niche—whether it's street performance, racing, or restoration. A solid supplier won't hesitate to share. Also, pay attention to how they handle questions: detailed, technical responses signal expertise; vague answers are a red flag. Longevity in the market often correlates with reliable casting and machining processes.
Insist on material certifications like A356 or 6061 alloy specs, and ask about their heat treatment protocols. If possible, visit the foundry or request third-party test reports. Reputable shops use spectroscopy to verify alloy composition. You want consistency—cheap heads often skimp on material purity, leading to cracks under thermal stress.
Look for ISO 9001 at a minimum; it shows process control. In motorsport circles, SAE or ASTM compliance adds weight. Some premium builders hold SFI specs or adhere to aerospace-level QC. But don't just tick boxes—ask how certifications translate to daily practice, like batch traceability and pressure testing each casting.
Precision CNC machining ensures port alignment, valve seat concentricity, and deck flatness. Ask about the equipment they use—5-axis mills are the gold standard. Request sample flow bench data; it reveals how well their CNC profiles perform. A capable supplier will share before/after CNC photos, not just final gloss.
Dig into their portfolio. Have they supplied heads for engines similar to yours—big-block Chevys, import turbos, or vintage flatheads? Look for dyno sheets from customer builds. Genuine shops often publish case studies or sponsor racers. Avoid those who only list generic “racing” without naming series, tracks, or engine builders they've worked with.
Overpromising on lead times or pricing that seems too low is a classic warning. Defensive reactions when you ask technical questions, lack of documentation for claims, or reluctance to provide photos of bare castings are all bad signs. Trust your gut: if they can't explain their core-flaw inspection process, walk away.
Local suppliers offer easier communication, shorter shipping, and simpler recourse if defects arise. However, some overseas foundries produce exceptional heads—especially if they cater to OEM or high-volume racing markets. The key is thorough vetting: request samples, check customs records for consistency, and factor in freight costs and duty. Don't assume 'local' automatically means better; many famous brands source castings globally.
It's critical. A confident supplier stands behind their work with a clear warranty that covers material and workmanship defects. Ask what the process looks like if a head arrives with porosity or a machining error. The best shops provide technical support during installation and tuning, not just a sales pitch. Good after-sales turns a transaction into a partnership for future builds.
Conclusion
Choosing an aluminum cylinder head supplier demands looking past glossy brochures to real craftsmanship. Inspect a head's port consistency, valve seat alignment, and surface finish—details that reveal a machine shop's pride. The metallurgy behind peak performance is equally critical; ask about the specific aluminum alloy blend, heat treatment cycles, and grain structure control. A supplier willing to share test data on material strength and thermal stability demonstrates a depth of engineering that separates true experts from mere parts resellers. This foundation in genuine craft and material science is what ensures your engine build will withstand extreme combustion pressures and thermal stress.
The best suppliers act as engineering partners, not just order-takers. They'll discuss your engine combination and suggest port designs, chamber volumes, or material enhancements that align with your power goals. Demand evidence of stress testing—thermal shock cycling, fatigue analysis, and real track hours—because a cylinder head's reliability is proven through abuse, not CAD animations. Look for dyno results and customer builds that mirror your intended use. Finally, gauge their commitment to lasting relationships: post-sale support, technical consulting, and a track record of iterative improvements based on user feedback. A supplier invested in your long-term success becomes a cornerstone of your engine program, not just a line item on a purchase order.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 8613967667688
Website: https://www.yongyu.com/