OEM Closed-Type Goggle Valve Essentials: Design Features and Industrial Uses
2026-07-11
In heavy industries where reliable gas shut-off is non-negotiable, the OEM closed-type goggle valve stands out as a critical component. Its unique design—featuring a robust, sealed spectacle plate—eliminates leakage risks even under extreme conditions, making it a staple in steel mills and chemical plants. As manufacturers push for tighter emission controls, understanding the nuances of these valves becomes essential. Leading the innovation is THT, whose decades of expertise have shaped modern goggle valve engineering. In this post, we'll unpack the core design elements and real-world applications that make closed-type goggle valves indispensable.
How Closed-Type Goggle Valves Control Flow with Precision
Closed-type goggle valves achieve precise flow regulation through a pair of spectacle-shaped plates that slide or rotate between the stream. One plate, the blank, fully blocks the passage, while the other, a ring or orifice, permits flow with minimal obstruction. The transition between open and closed positions is gradual, allowing operators to throttle the media by adjusting the overlapping area between the plates. This design eliminates the sudden pressure surges common with gate valves, enabling smooth modulation even with viscous or particulate-laden fluids.
The sealing mechanism further refines control, as the plates press against resilient seats under mechanical or hydraulic force. When partially open, the asymmetrical flow path creates a Venturi effect, stabilizing the velocity profile and reducing turbulence. Engineers can calibrate the actuation system—whether manual, pneumatic, or electric—to respond in fine increments, often using positioners that accept analog or digital signals for real-time adjustments. Such precision is valuable in dosing applications, where a fraction of a millimeter in plate displacement correlates to a predictable change in flow rate.
Maintenance of accuracy over time is ensured by the valve’s enclosed body, shielding internal components from dust, moisture, and corrosive atmospheres. The spectacle plates can be hard-faced or coated with ceramics to withstand erosion and maintain their geometric integrity. Even after thousands of cycles, the valve repeats its performance with negligible drift, partly because the actuating mechanism operates on a simple, robust linkage. In critical processes—like reactor feed lines or cooling water circuits—this combination of mechanical simplicity and refined control makes closed-type goggle valves a reliable choice for demanding environments.
Core Design Innovations in OEM Goggle Valve Models
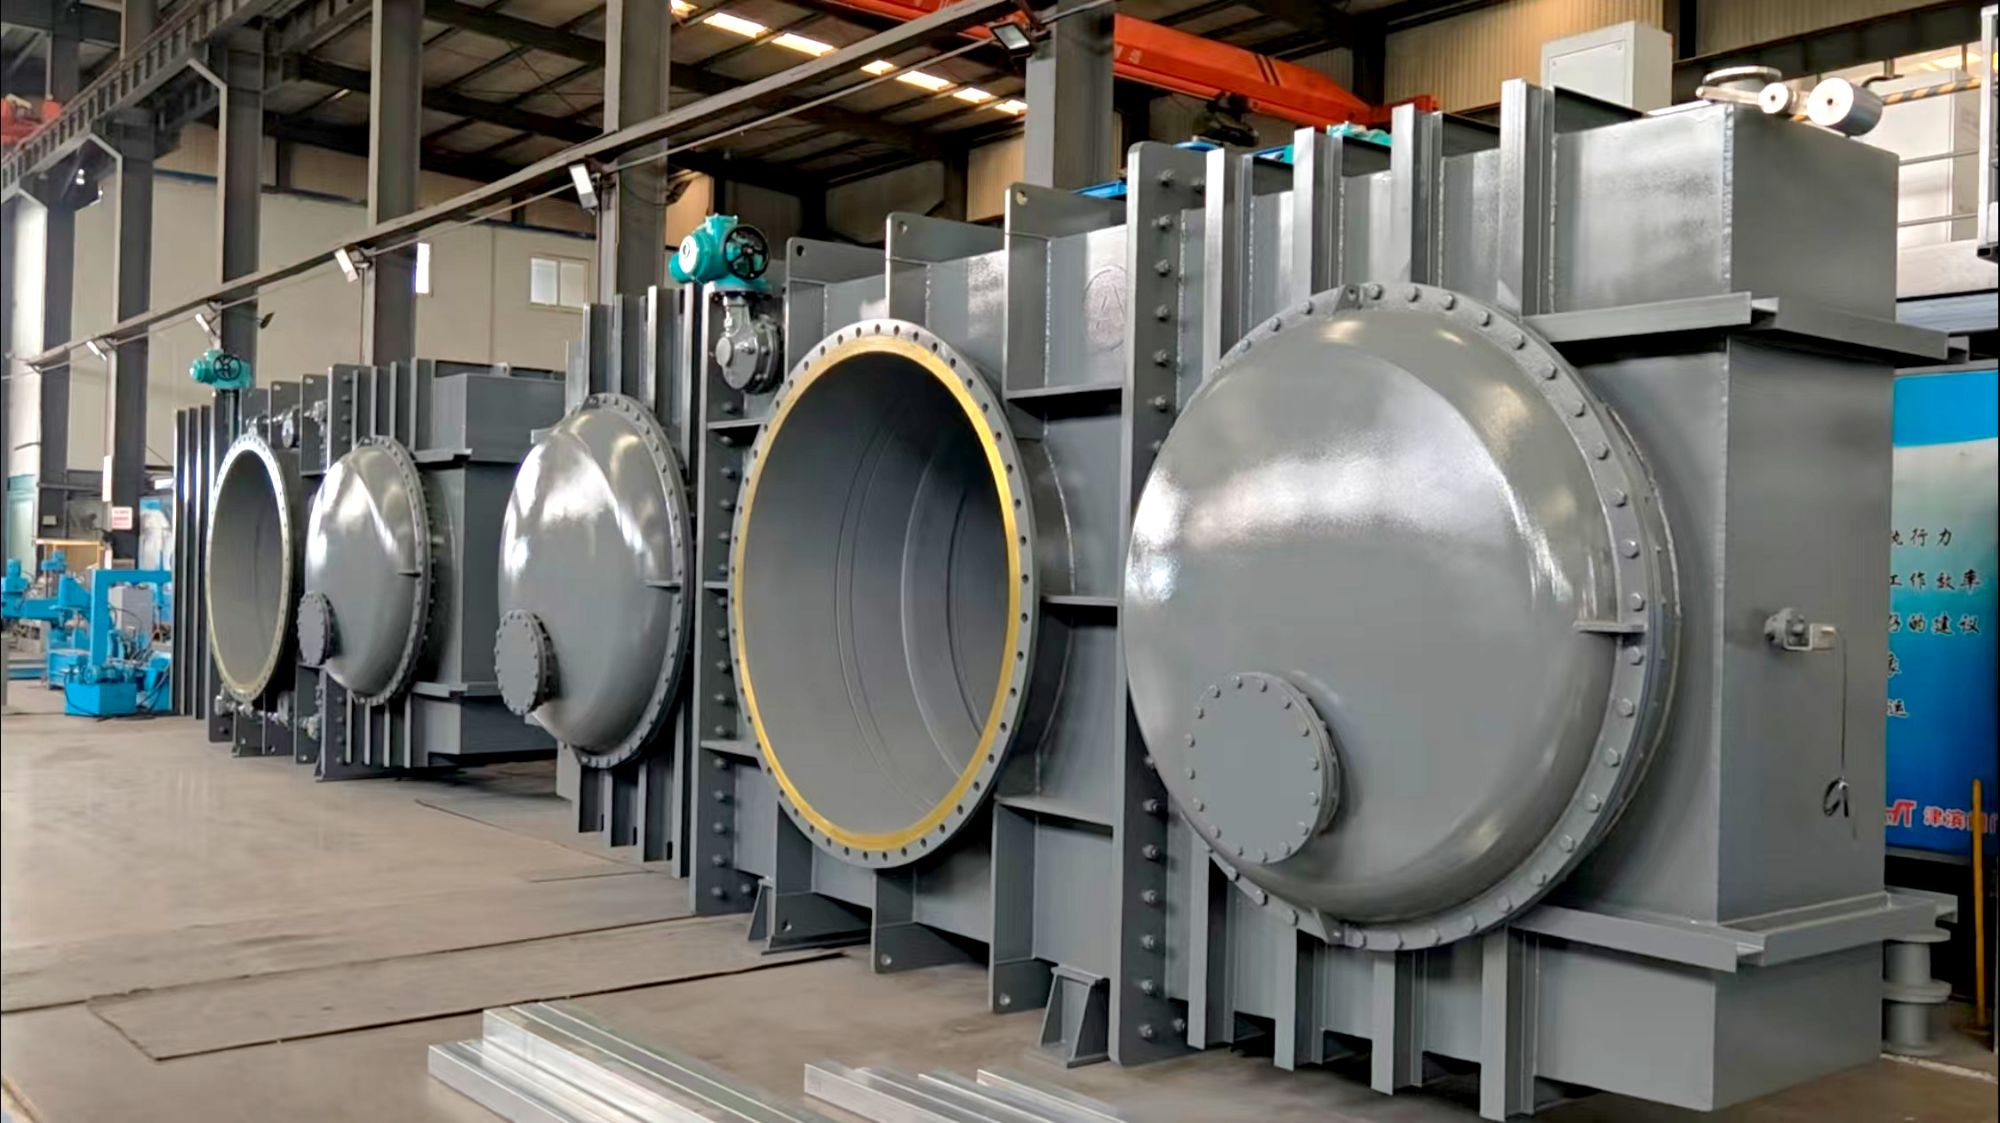
The latest OEM goggle valves have undergone a quiet but significant transformation in how they manage solids flow. Instead of relying solely on traditional sliding gate mechanisms, engineers have introduced segmented blade assemblies that create a more controlled shutoff. These blades move in a staggered sequence, reducing the sudden pressure spikes that often cause wear in high-temperature processes. The result is a valve that closes smoothly without sacrificing the tight seal required in refining and petrochemical environments.
Another shift is found in the actuation system. Pneumatic cylinders have been repositioned to align with the valve body in a way that minimizes lateral stress on the stem. This subtle realignment, combined with self-lubricating bushings at pivot points, means field technicians spend less time on greasing routines. Some models now feature a quick-access panel that exposes the entire linkage without unbolting the bonnet, cutting inspection downtime by half in many cases.
Material upgrades have also played a role, but the thinking here is more nuanced than simply switching to exotic alloys. Rather, designers are using dual-hardness overlays on the seating surfaces—hard where abrasion hits hardest, yet ductile enough elsewhere to absorb thermal expansion cycles. It’s a balanced approach that extends service life without inflating cost, and one that reflects a deeper understanding of how these components actually degrade in the field.
Selecting the Right Materials for Harsh Operating Conditions
In environments where temperature swings, corrosive chemicals, or abrasive media are the norm, material choice becomes less about preference and more about survival. The first step is a brutally honest audit of every stressor a component will face—not just the obvious ones like acid splashes or high heat, but also the subtle, cumulative factors like thermal cycling, vibration, and even UV exposure. Overlooking these can turn a well-intentioned spec into an expensive failure. For instance, a stainless steel that laughs off a caustic rinse at room temperature might crack open under chloride stress at 80°C, a detail that only emerges when you dig into the specific grades and their real-world limits.
Beyond basic chemical compatibility, the interplay between mechanical demands and environmental attack often dictates the winner. In subsea oil and gas equipment, the material must not only resist hydrogen sulfide embrittlement but also handle extreme pressures without deformation. That dual requirement has driven the development of specialized nickel alloys and duplex stainless steels, which balance strength and corrosion resistance in ways that standard off-the-shelf options cannot. Even then, small tweaks in heat treatment or surface finish can make a night-and-day difference in service life. This is where collaboration with metallurgists and field engineers pays off, turning laboratory data into practical, long-lived solutions.
Sometimes, the right material isn’t the most exotic one but the one applied with a clever engineering twist. In mining slurry applications, plain carbon steel lined with a thick rubber or ceramic coating can outperform a solid high-chrome alloy because the liner absorbs impact and wear in a way a monolithic metal never could. Similarly, in semiconductor manufacturing, ultra-high-purity polymers like PFA replace metal entirely, eliminating contamination risks while handling aggressive etchants. The common thread is a willingness to look past initial material cost and focus on the total cost of ownership—factoring in maintenance downtime, replacement frequency, and safety margins. That shift in perspective often reveals that the “cheaper” material is anything but.
Typical Industrial Scenarios That Rely on These Valves
In oil and gas extraction, high-pressure choke valves are placed on wellheads to regulate flow from reservoirs that can surge unexpectedly. Without them, the sudden release of hydrocarbons would overwhelm downstream separators and flare systems, creating serious safety hazards. These valves often operate in remote, unmanned locations, so their reliability isn’t just about performance—it’s a direct factor in preventing environmental incidents.
Chemical processing plants depend on precision metering valves to blend raw ingredients at exact ratios. A slight deviation in flow rate could ruin an entire batch or trigger a runaway reaction. Alloy selection becomes critical here because aggressive media like chlorine or sulfuric acid can eat through standard materials within weeks, leading to leaks that halt production and rack up cleanup costs.
Power generation cycles push valves to their thermal limits. Combined-cycle plants, for example, rely on fast-acting bypass valves to protect gas turbines during trips—they must slam shut within milliseconds to divert superheated steam, then reopen smoothly without causing water hammer. The constant thermal cycling demands designs that can handle expansion and contraction without jamming or cracking over decades of service.
Maintenance Advantages That Reduce Downtime
Real-time equipment monitoring has completely changed how we approach system reliability. Instead of waiting for something to break, sensors and analytics flag subtle performance shifts long before they become failures. This means repairs can be scheduled during planned slow periods, not in the middle of peak demand. The result is far less unplanned downtime and a maintenance team that works proactively rather than constantly fighting fires.
Another quiet game changer is the move toward modular components and hot-swappable parts. When a critical piece of hardware can be replaced without shutting down the entire line, repairs that used to take hours now take minutes. It’s a design philosophy that puts uptime first, and it eliminates the scramble to find temporary workarounds or extended outages that frustrate both operators and customers.
Standardizing maintenance protocols across similar equipment also pays dividends. When technicians have clear, consistent steps to follow—backed by digital checklists and updated reference guides—diagnosis and repair times shrink dramatically. Less guesswork, fewer repeat visits, and a growing institutional knowledge base mean problems get solved right the first time, keeping operations humming without interruption.
Built-In Safety Mechanisms for Reliable Shutoff
Modern industrial control systems embed multiple layers of protection to ensure that a shutoff command is executed without exception. These mechanisms are not reliant on software logic alone; they often include dedicated hardware pathways that physically interrupt power or signal flow when triggered. For example, a safety relay with force-guided contacts can provide a direct, hardwired disconnect that overrides any processor state, ensuring that even if the main controller malfunctions, the shutdown sequence completes reliably.
Beyond hardware interlocks, built-in redundancy plays a crucial role. Dual-channel architectures compare signals from independent sensors and actuators, and any discrepancy immediately forces a safe-state cutoff. This cross-verification eliminates single points of failure, which is especially critical in high-risk environments like chemical processing or nuclear facilities. The decision to shut down is not delegated to a single component but emerges from a consensus among multiple, diverse elements, making spurious or missed trips far less likely.
Another key aspect is the use of stored energy systems that maintain shutoff capability even during total power loss. Spring-return actuators, fail-safe braking mechanisms, and capacitor-backed trip circuits guarantee that the protective action does not depend on continuous external supply. This design philosophy means that the safety function is always available, even under the most adverse conditions, and it aligns with international standards that demand failure mode analysis to favor the safe state.
FAQ
An OEM closed-type goggle valve is built to exact specifications provided by the end user or equipment manufacturer, ensuring seamless integration into existing systems. Unlike off-the-shelf standard valves, these feature a fully enclosed spectacle plate mechanism that prevents external contamination and provides a clear visual open/closed indicator, enhancing both safety and reliability in demanding environments.
The closed-type design completely houses the spectacle plate, eliminating exposure to personnel and the environment during operation. This containment reduces the risk of accidental contact with fluid media, prevents leakage even under pressure surges, and ensures that the valve position is unmistakably visible, which is critical for lockout/tagout procedures and maintenance safety.
Key features include a robust body casting that resists thermal distortion, precisely machined seating surfaces for tight shut-off, a swing-through spectacle plate that minimizes turbulence, and a self-aligning mechanism that maintains seal integrity over thousands of cycles. Many OEM designs also incorporate blowout-proof stems and anti-static devices for added reliability.
They see extensive use in the oil and gas sector, petrochemical processing, power generation, and steel manufacturing. Anywhere that demands absolute downstream isolation—such as furnace fuel lines, reactor feed systems, or high-temperature steam networks—these valves are preferred for their ability to handle aggressive media and provide full-bore flow with minimal pressure drop.
Body materials range from carbon steel and stainless steel to high-grade alloys like Hastelloy, selected based on the service temperature and corrosive nature of the fluid. Seats and seals often employ reinforced PTFE, graphite laminate, or metal-to-metal configurations. Trim components are frequently hardened or coated with Stellite to resist wear in abrasive applications.
In an open-type goggle valve, the spectacle plate moves in an exposed area where debris can accumulate and hamper sealing. The closed-type encloses the entire mechanism, protecting it from dirt and weather. The enclosed cavity also allows for a secondary containment feature, such as a purge port that maintains a clean sealing environment and immediately reveals any internal bypass through a telltale leakoff connection.
Absolutely. OEMs offer extensive customization including special face-to-face dimensions to match existing pipework, exotic materials for extreme corrosion resistance, actuation options (manual gear, electric, pneumatic), and custom coatings for subsea or arctic service. Intelligent position sensors and partial-stroke testing capabilities can also be integrated for safety instrumented systems.
Regular inspection of the spectacle plate and seat surfaces for erosion is crucial, along with lubrication of the hinge pin and actuator mechanism per manufacturer guidelines. The enclosed cavity should be periodically purged of any accumulated condensate, and seat rings should be re-lapped if minor leakage develops. For valves in intermittent service, exercising the valve through a full cycle every few months prevents stiction and ensures emergency readiness.
Conclusion
OEM closed-type goggle valves are engineered to deliver precision flow control through a robust shut-off mechanism that completely isolates process media. A sliding spectacle plate, featuring a solid blank and an open ring, moves between flanges to either permit or block flow. This design minimizes leakage points and provides a tight seal, essential in applications demanding absolute isolation to prevent cross-contamination or hazardous releases. Core innovations include reinforced plate guides, enclosed bonnets that protect moving parts from debris, and actuator options—manual, pneumatic, or hydraulic—that enable precise positioning even under high-pressure differentials. The enclosed structure inherently shields the valve internals, extending service life in dusty or wet environments.
Material selection is fundamental to performance under harsh conditions, with bodies typically cast from ductile iron, carbon steel, or stainless steel, and seats available in PTFE, Viton, or metal for chemical and temperature resilience. These valves thrive in mining slurries, chemical processing, power plant ash handling, and wastewater treatment, where reliability and zero fugitive emissions are critical. Maintenance is simplified through replaceable seat rings and clear visual position indicators, reducing downtime during inspections. Safety is further bolstered by lockout provisions and fire-safe compliance, ensuring a fail-safe shutoff that operators can trust. The fusion of rugged construction, adaptable actuation, and low lifecycle costs makes these valves a distinctive choice for engineers seeking dependable isolation in demanding industrial settings.
Contact Us
Contact Person: Su Zhang
Email: [email protected]
Tel/WhatsApp: +86-25219206
Website: https://www.tht-valve.com/