Professional Corrugated Box Die Making Creasing Cutting Machine: Essential Guide for Manufacturers
2026-08-19
Every carton that reaches a customer starts with a die-making decision most manufacturers overlook. If your creasing and cutting machine can't hold tolerances, you're not just wasting board—you're burning margin on every run. That's where ADEWO changes the equation: professional corrugated box die making and creasing cutting systems built for the pressures of real production floors. This guide cuts through the noise to show what actually matters before you invest.
How Creasing Depth and Rule Selection Affect Box Fold Quality
Creasing depth works like a controlled fracture line. If the rule cuts too shallow, the outer liner stretches beyond its elastic limit during folding, which shows up as rough, cracked edges—especially on recycled boards or heavy clay-coated sheets. Push the crease too deep, and the board loses too much of its structural core, leaving the fold wobbly and prone to splitting along the score. Getting the right depth means the crease groove deforms the fibers just enough to create a hinge without breaking the surface tension of the liner.
Rule selection matters just as much as the depth setting. A thin rule on a thick corrugated or solid board will bottom out and bruise the sheet before it forms a clean channel, while an overly wide rule on lightweight stock can crush the crease instead of defining it. Matching rule width, profile, and hardness to the caliper and fiber direction keeps the fold resistance consistent. When the rule is slightly narrower than the creasing matrix channel, the board folds along a predictable line with less spring-back and fewer fiber tears at the corners.
Inside the Cutting Unit: Key Components That Determine Longevity
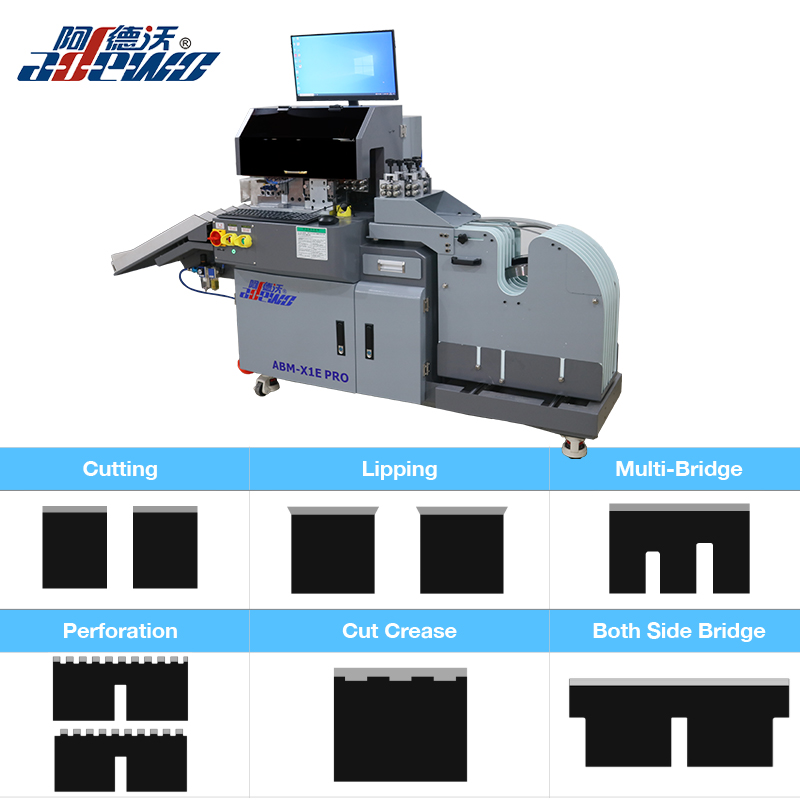
The spindle assembly sits at the heart of any cutting unit, and its bearings are the first place wear shows up. A cheap sealed bearing might survive one season of fine dust and damp grass, but once moisture sneaks past the shield, the grease breaks down and you get that telltale whine before failure. Look for spindles with double-lipped seals or a grease fitting that lets you push out contaminants rather than trapping them inside. The blade mount matters just as much—a hardened steel boss with a precise pilot keeps the blade from wobbling, which would otherwise hammer the bearing races into an early grave.
Drive components rarely get the attention they deserve until a belt snaps mid-cut. A well-built deck uses a spring-loaded idler that maintains constant tension without overloading the spindle bearings, while cheaper designs rely on a fixed idler that lets the belt slip and glaze. The pulleys themselves should be machined rather than stamped; a rough groove chews through belts and sends rubber dust into every bearing nearby. If the unit runs a gearbox instead of belts, check whether the gears are cut or sintered—cut gears hold their tooth profile longer under shock loads like hitting a hidden root.
The deck shell ties everything together, and its failure is usually a slow, rust-driven process. Stamped steel decks with minimal reinforcement flex under load, cracking around the spindle mounts after a few hundred hours. Thicker gauge steel or added stiffening ribs delay that fatigue, but the real killer is debris trapped against bare metal. A quality unit routes clippings away from the spindle housings and leaves no flat ledges where wet grass can sit. Powder coating or an e-coat primer underneath the paint matters more than the color on top—once rust starts under the finish, it spreads unseen until a spindle breaks loose.
Choosing the Right Automation Level Without Overpaying for Unused Features
Many teams fall into the trap of buying an automation platform with every possible module, only to realize months later they are using a fraction of what they paid for. A better starting point is to map out the tasks that are genuinely repetitive, time-consuming, or prone to human error. Once you have that list, you can match each need to a specific automation capability instead of paying for a bloated suite.
It also helps to look for tools that let you activate features as you go. Some vendors lock advanced workflows behind higher pricing tiers, but others offer add-ons or usage-based models that scale with actual demand. Before adding a premium plan, ask whether the extra functionality will be used in the next quarter. If the answer is no, it is probably not worth the cost.
Finally, review your automation footprint regularly. Teams sometimes automate for the sake of automation, bringing simple one-off tasks into a system that now requires ongoing maintenance. Keeping the scope aligned with real operational needs is the most reliable way to balance efficiency and budget.
Daily, Weekly, and Monthly Maintenance Routines for Reliable Operation
Make the morning walk-around a habit. Even five minutes spent checking for oil spots, loose hoses, or unusual vibrations can save a full shift of downtime later. Top up fluids only if the level has genuinely dropped; sudden losses deserve a closer look, not just a refill.
Set aside half an hour midweek for the tasks that tend to get skipped. Wipe down air intakes, give grease fittings a few pumps, and run the emergency stop test while the machine is under light load. Check belt tension with your thumb—if it gives more than a quarter inch, snug it up.
Once a month, go deeper than the quick checks. Replace filters and belts that are nearing the end of their service life, even if they still look okay. Pull the covers and blow out dust from cooling fins and electrical cabinets. Torque the main terminal screws and inspect contactors for pitting. Use the monthly log to spot patterns: a slowly rising temperature or increasing vibration often points to a problem that won't wait for the next scheduled overhaul.
Fixing Common Defects: From Cracked Creases to Incomplete Cuts
Cracked creases usually mean the material is being forced to fold along a line that hasn't been properly weakened. Instead of increasing pressure right away, check the creasing channel width against the stock thickness. A channel that's too narrow pinches the fibers and causes them to split along the fold, while too wide a channel creates a sloppy fold line with no crispness. Try switching to a shallower creasing rule or applying a light pre-score pass on heavy or coated boards. For plastics and dense paperboards, warming the sheet slightly before creasing can relax the surface enough to prevent hairline fractures.
Incomplete cuts often show up as ragged edges or hanging fibers that didn't separate fully. This rarely means the blade is broken; more often the cutting rule has lost its edge or the bed has worn unevenly under repeated runs. Swap in a fresh blade for one job and see if the problem disappears. If it persists, place a sheet of carbon paper between the material and the cutting die to reveal low-pressure zones. You can shim those areas with thin tape rather than cranking up overall force, which risks crushing the stock elsewhere.
A practical habit is to keep a small notebook next to the cutting machine. Note the material brand, thickness, crease channel size, blade depth, and pressure reading for every successful job. When a new defect shows up mid-run, you can compare against past settings and pinpoint what drifted. Most defects trace back to a dull tool, a dirty platen, or a material batch that behaves slightly differently from the previous one—catching the change early saves a full stack of ruined blanks.
Signs It’s Time to Upgrade Your Die Making Machine
When your die making machine starts demanding repairs more often than it produces parts, that's a clear signal. Downtime creeps up, delivery dates slip, and your maintenance budget balloons without any real improvement in output. If you're calling the technician every other week just to keep the line moving, you're not running a production shop anymore—you're running a repair bay.
Another telling sign is when the machine can't hold tolerances it once nailed without a second thought. Parts come out with slight variations that force rework or scrap, and newer die designs simply won't run on the old control system. You might also notice that finding spare parts has turned into a scavenger hunt, and the software is so outdated that your operators have to invent workarounds just to get a basic job done. That's not a small inconvenience; it's the machine telling you it's past its useful life.
FAQ
It handles the precision work of scoring and cutting corrugated board so that flat sheets fold cleanly into boxes. Instead of relying on manual templates, the machine uses a die to press crease lines and cut profiles in one pass, which keeps production consistent.
Professional models are built for higher volumes and tighter tolerances. You get less edge crushing, cleaner creases, and the ability to swap dies quickly for different box sizes. Over time, that reduces waste and the need for rework, especially if you're running multiple shifts.
Look at the maximum sheet size, creasing depth control, die locking system, and how easy it is to adjust pressure. Also check whether it handles double-wall or triple-wall board if that's part of your product range. A good safety system and accessible maintenance points matter more than flashy extras.
Creasing compresses the board along a line so the fibers fold without cracking, while cutting shears through the material completely. Good machines let you set crease depth and cutting pressure independently, which is crucial for different flute types.
Daily cleaning of paper dust, regular inspection of die bolts, and lubrication of moving guides. The creasing matrix and cutting plate wear over time, so check them weekly for flat spots or grooves. Don't wait until cuts get ragged—replace consumables on a schedule.
It depends on the control interface. Modern machines often have touchscreen settings with saved job recipes, so an operator can load a previous setup in minutes. The main learning curve is understanding how board thickness and flute profile affect pressure settings, which comes with hands-on practice.
Yes, if the die bed is large enough and the machine offers fine pressure control. Complex displays need more intricate dies and sometimes multiple crease depths, so check that the machine supports quick die changes and precise depth adjustment.
Conclusion
Getting consistent, clean folds from a corrugated die making creasing and cutting machine starts well before the first sheet runs through. Creasing depth and rule selection are not interchangeable settings; they shape how the board bends, and getting them wrong leads to cracked creases or weak hinges. At the same time, the cutting unit deserves closer attention than it often receives. Wear-prone parts like anvils, chase plates, and cutting dies dictate how long the machine holds its accuracy. Spending on higher automation rarely pays off if you are only running standard box styles, so buyers should match servo-driven features to actual production mix instead of chasing unused capabilities. A manual or semi-automatic setup can be the smarter choice for a narrow range of repeat jobs, while fully automated lines earn their keep in high-mix environments.
Operational reliability comes from a maintenance rhythm that many shops overlook until something breaks. Daily checks on lubrication and cutting pressure, weekly inspection of rule height and bearing play, and monthly deep cleaning of the cutting unit prevent most unplanned downtime. When defects do appear—cracked creases, incomplete cuts, or uneven pressure—start with the simplest adjustments before replacing tooling. Often a slight rule depth change or pressure rebalancing solves the issue without expensive parts. If you find yourself constantly chasing alignment, patching worn anvils, or rejecting finished sheets for the same recurring flaws, those are clear signs the machine has outlived its economic life. Upgrading should be driven by repeat failure patterns and shifting order profiles, not just equipment age. The right guide for manufacturers treats the machine as a system where creasing, cutting, automation, and maintenance decisions are connected, not isolated choices.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com