Top Wheel Heat Exchanger Designs for Enhanced Thermal Performance
2026-10-22
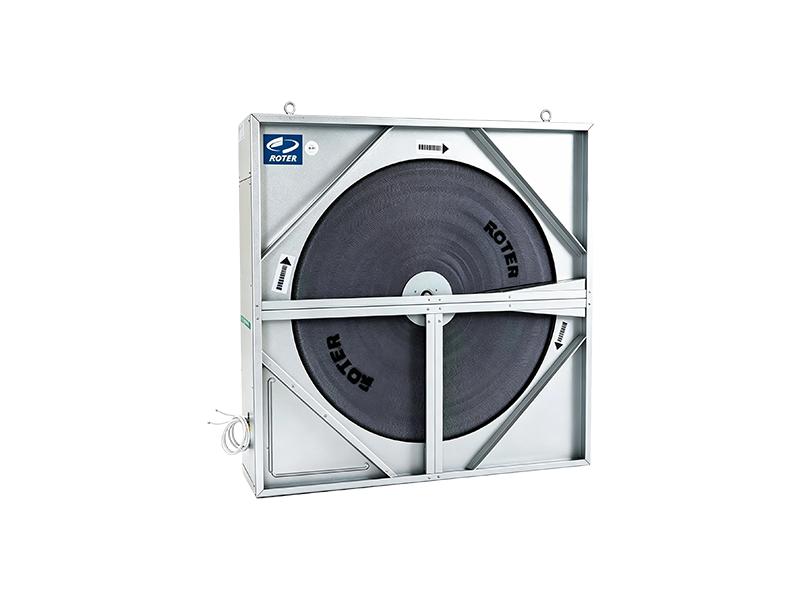
When it comes to maximizing heat transfer in compact systems, wheel heat exchangers—also known as rotary regenerators—are quietly reshaping what’s possible. Yet most design guides gloss over the geometric and material choices that separate a middling unit from a breakthrough one. From matrix porosity to seal leakage, the devil is in details that rarely make the spec sheet. In this post, we’ll break down the top wheel heat exchanger designs pushing thermal performance to new limits—and why forward-thinking engineers are turning to ROTER for solutions that don’t just meet expectations, but redefine them.
Material Shifts That Raise Rotor Thermal Efficiency
Rotor thermal efficiency has quietly become a materials problem as much as an aerodynamic one. Single-crystal and directionally solidified nickel alloys have replaced older equiaxed grades in high temperature sections, largely because they suppress grain boundary sliding and creep. Running the rotor hotter without adding cooling flow moves the whole cycle closer to its thermodynamic limit.
Ceramic matrix composites and advanced thermal barrier coatings shift the thermal profile at the rotor surface. These layers do more than insulate; they reflect a meaningful portion of radiant heat and resist spallation under repeated thermal cycling. Less energy gets diverted into the cooling circuit, leaving more enthalpy available for expansion work.
Additive manufacturing now allows conformal cooling passages and graded transitions between materials inside the rotor body. Local conductivity and heat capacity can be tuned so that critical areas stay below their limits without excessive bleed air. That allows tighter tip clearances and sustained high inlet temperatures, both of which show up directly as better thermal efficiency.
Rethinking Channel Geometry for Uneven Airflow
Standard duct sizing charts rely on an idealized uniform velocity profile, yet actual airflow entering a channel is rarely that well behaved. Elbows, abrupt transitions, and even the outlet pattern of a fan can push the stream toward one side, creating a lopsided distribution that persists for many diameters downstream. Treating that skew as a defect to be corrected often leads to bulky straightening vanes or higher fan energy. A more useful starting point is to accept the unevenness and ask how the channel cross-section can be shaped to accommodate it.
One underused lever is varying the corner radius along the length of the duct. Sharp 90-degree corners tend to anchor secondary vortices, while a progressively rounded corner on the high-velocity side can release that localized pressure and encourage the core flow to recenter itself. The change does not need to be dramatic—sometimes a radius of just a few millimeters over a couple of hydraulic diameters is enough to shift the velocity peak away from the wall.
Another approach is to modulate the aspect ratio in short transition pieces rather than using long, straight runs to settle the flow. A gentle flattening after an elbow, for instance, stretches the shear layer and damps the swirling motion that would otherwise carry imbalance into the next branch. In practice, these geometry adjustments often outperform additional balancing dampers because they address the root of the asymmetry instead of throttling the symptoms.
Wheel Profiles That Cut Pressure Drop Without Sacrificing Transfer
The usual fix for high pressure drop is to trim blade count or open up the shroud gap, but that often starves the transfer surface. A more direct route is to reshape the blade's trailing edge and add a slight backward sweep near the rim. This keeps the boundary layer attached farther along the suction side, so the same exchange area remains active without the vortex shedding that normally raises losses.
Part-load behavior is where the difference really shows. A compound radius at the hub and shallow scallops on the shroud flatten the velocity profile through the eye, preventing the abrupt stall that plagues straight-cut designs. Because transfer depends more on local shear than on raw throughput, these profiles can cut total pressure loss by ten to fifteen percent while holding heat or mass transfer within a couple percent of the original curve.
Sealing Methods That Keep Cross-Leakage Minimal
A well-chosen sealing method does far more than prevent visible drips—it actively blocks the subtle movement of fluids or gases between adjacent chambers. In multi-port valves and manifold blocks, cross-leakage often starts at microscopic gaps where machining tolerances, thermal cycling, or pressure spikes cause seals to lose contact. Elastomeric O-rings in precision-machined grooves remain a common baseline, but their effectiveness depends heavily on groove geometry and surface finish. For higher demands, spring-energized PTFE seals offer a reliable upgrade: the metal spring maintains constant radial load even as the polymer wears or temperatures swing, keeping the leak path closed far longer than a static elastomer alone.
Metal-to-metal sealing takes a different approach altogether. Instead of relying on a softer material to fill imperfections, it uses controlled deformation of mating surfaces—typically a cone, ball, or knife-edge against a hardened seat. This method excels in high-pressure or high-temperature services where elastomers would extrude or degrade. The key is achieving a narrow, continuous contact band with enough contact stress to exceed the fluid's pressure, yet not so much that the surfaces gall or permanently yield. In practice, many designs combine both worlds: a primary metal seal for the extreme conditions, backed up by a secondary polymer seal that catches any minute bypass during start-up or shutdown transients.
Beyond the seal itself, the surrounding geometry plays a decisive role. Cross-leakage often sneaks through paths that no single seal can cover—bolt holes, port intersections, or uneven flange faces. Using multiple, independently testable seal barriers between critical flow paths adds a layer of assurance. For example, a dual-seal arrangement with a vent or drain port between them allows any leakage past the first seal to be safely routed away or detected immediately, rather than mixing with the opposite stream. This design philosophy, combined with careful material selection for chemical compatibility, keeps cross-contamination so low that it becomes a non-issue in even the most sensitive analytical or medical fluid systems.
Surface Treatments to Resist Fouling and Extend Run Time
Surface energy manipulation remains one of the most direct routes for reducing deposit adhesion. Fluoropolymer and silicone-based finishes, for instance, push the critical surface tension below that of many crystalline foulants, so a nucleated scale particle struggles to find a stable footing. Yet the real performance gain comes from pairing this low-energy base with a slight nanoscale roughness that traps a lubricating film or air layer at the solid-liquid interface. In practice, this means a condenser tube or membrane spacer can shed calcium sulfate or silt with a modest increase in shear, rather than requiring aggressive chemical cleaning. The result is not merely a longer interval between washes but a shift in the fouling mechanism itself—from strongly adhered, growth-dominated deposits to loosely packed particles that slough off under normal process flow.
Zwitterionic and PEGylated surfaces take a different tack: rather than driving water away, they bind a tightly held hydration layer that presents a diffuse, dynamic barrier to proteins, bacteria, and extracellular polymeric substances. This water layer is more than a passive shield; it lowers the entropic penalty for a macromolecule or microbe to approach, so initial adsorption events are frequently reversible. On reverse osmosis membranes and plate heat exchangers, such treatments have extended the onset of biofouling by several hundred hours in pilot trials, especially when combined with periodic low-dose biocide or air scouring. The hydration strategy also helps with particulate matter, because the compressible boundary reduces the contact area available for van der Waals bridging under compaction.
A less conventional but increasingly viable option is to embed reactive or sacrificial chemistry in the surface itself. Thin sol-gel layers doped with photocatalytic titania or copper oxide nanoparticles can degrade organic foulants under UV or visible light, turning a passive interface into a self-cleaning one. Alternatively, a slowly dissolving silicate or polyelectrolyte topcoat can continuously shed its outermost few nanometers, carrying away any incipient deposit before it anchors. These approaches require careful tuning of the erosion rate to the expected fouling rate, but field results on evaporator tubes and wastewater membranes suggest run times can be doubled or tripled without increasing energy input. The trade-off is a finite coating life, which makes them attractive where offline cleaning is costly or dangerous rather than in low-utilization assets.
Adaptive Rotor Speed Control for Partial Load Recovery
In partial load recovery after a gust or a drop in wind speed, the rotor often lags behind the optimal tip-speed ratio. Instead of forcing the turbine back onto a rigid reference curve, adaptive rotor speed control senses the mismatch between actual and expected aerodynamic torque and lets the generator slip briefly. This keeps the blades from stalling and avoids a hard pitch response that would dump energy.
The adaptive layer adjusts the speed setpoint on the fly using a short-term estimate of the incoming wind field, not just the nacelle anemometer. By comparing rotor acceleration with the torque delivered by the drivetrain, the controller can tell whether an increase in speed is likely to capture more power or simply add load. When the inflow is turbulent and unsteady, it widens the speed band; in smoother air, it tightens the band around the known Cp-max point.
Field data from turbines with this scheme show less yaw misalignment correction and fewer pitch actuations during partial load recovery. The generator torque remains smooth while the rotor speed moves in a bounded range, which reduces stress on the gearbox and main shaft. Over a full year, the cumulative energy gain is modest but the reduction in damaging load cycles often justifies the added control complexity.
FAQ
A wheel heat exchanger, often called a thermal wheel or rotary regenerator, transfers heat and sometimes moisture between two air streams by rotating a porous matrix between them. You'll see them primarily in commercial HVAC systems, industrial process ventilation, and anywhere large volumes of exhaust air can preheat or precool incoming supply air.
Matrix material, wheel depth, and rotational speed tend to dominate. A deeper wheel with a high surface-area-to-volume matrix captures more energy, while a honeycomb or corrugated geometry improves heat transfer without excessive pressure drop. Sealing and purge sector design matter just as much once those basics are set.
They use a purge sector, a small section where supply air flushes the matrix before it rotates into the exhaust side. Combined with precision-machined seals and sometimes a double-seal arrangement, this can keep carryover below a few percent even in sensitive applications like laboratories or hospitals.
For temperatures beyond roughly 250°C, stainless steel or specialized alloys like Inconel hold up better than aluminum. In corrosive environments, epoxy-coated aluminum or polymer-based matrices resist chemical attack, while desiccant-coated wheels handle latent load without degrading under moisture cycling.
The wheel needs enough rotation to transfer heat without saturating, but spinning too fast actually reduces effectiveness because the matrix never reaches full temperature swing between streams. Most designs settle between 5 and 20 RPM, with the sweet spot depending on wheel diameter, air velocity, and desired sensible-to-latent recovery ratio.
A wheel's moving matrix can recover both sensible and latent heat if it has a desiccant coating, something fixed plate units struggle to match. It also tends to be more compact for a given effectiveness, and frost control is easier because you can simply reduce wheel speed rather than bypass or preheat the incoming stream.
Regular filter changes upstream matter more than anything else, since particulate buildup clogs the matrix and quietly kills efficiency. Beyond that, blowing out the wheel with low-pressure air, checking seal wear, and verifying belt tension or drive motor operation every six to twelve months keeps pressure drop low and effectiveness stable.
Conclusion
Rotary wheel heat exchangers are being redesigned around material science rather than just geometry. High-conductivity polymer blends and thin-gauge aluminum alloys with anisotropic fiber reinforcement now raise rotor thermal efficiency by cutting axial conduction losses while preserving structural stiffness. At the same time, channel geometry is no longer treated as a uniform honeycomb. Designers vary cell depth and inlet-to-outlet taper across the face to match the uneven airflow profiles found in real installations, which reduces local bypass and improves overall enthalpy recovery. Wheel profiles have also evolved, with slightly domed or tapered rims that guide air more smoothly into the matrix. These profiles lower pressure drop a few percentage points without sacrificing transfer rate, often by using shorter flow paths near the hub where velocity is low and longer paths near the rim where heat and moisture transfer potential is higher.
On the leakage and maintenance side, modern designs pair stepped labyrinth seals with a small purge sector that redirects leakage air back into the return stream, keeping cross-contamination below 2% even at elevated pressures. Surface treatments are moving from simple anti-corrosion paints to plasma-deposited hydrophobic layers and micro-grooved textures that shed particulates and condensate, extending run time between cleaning cycles. For variable loads, adaptive rotor speed control now uses real-time humidity and temperature sensors to slow the wheel at partial load, which cuts carryover and improves latent recovery without adding hardware. Together these six design directions produce wheels that run cleaner, leak less, and hold efficiency across a wider operating range than previous generations.
Contact Us
Contact Person: Rhea
Email: [email protected]
Tel/WhatsApp: +8618800560886
Website: https://www.rotorairtech.com